Malaysia Steel Service Centre Starts Up Continuous Hot Dip Galvanizing Line for 200,000 MT Annual Output
A Malaysian steel service centre has successfully commissioned a continuous hot-dip galvanizing production line with an annual capacity of 200,000 MT, ending its long dependence on imported galvanized coil. The line now supplies CQ, DQ and DDQ grade GI coil to construction, HVAC, appliance and general fabrication customers across Peninsular Malaysia and the wider ASEAN market.
Client Background
The client is a steel coil processing and distribution business operating a service centre near Port Klang. For years it bought cold-rolled and galvanized coil from overseas mills, slit and cut it to size, and delivered to local manufacturers. Rising freight costs, volatile import pricing and lead times of eight to twelve weeks made it increasingly difficult to serve customers who needed fast, predictable replenishment of galvanized material.
The Challenge
- No in-house galvanizing capability — every tonne of GI coil had to be imported
- Long import lead times and currency exposure squeezed margins and slowed delivery
- Customers required a full grade range, from commercial quality to deep-drawing quality
- Coating weight had to be held within tight tolerances for downstream forming and painting
- High energy consumption of a galvanizing furnace threatened operating costs
The Solution
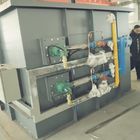
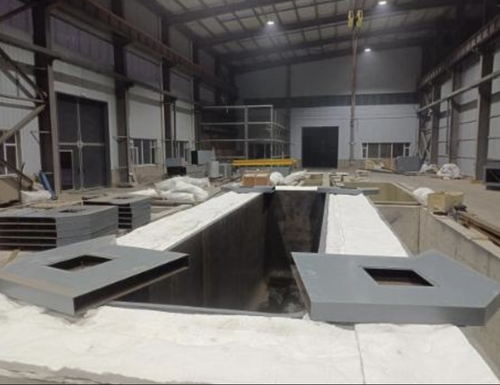
We supplied a complete continuous hot-dip galvanizing line engineered to coat a layer of zinc (or zinc-aluminium alloy) onto the strip at high temperature in a single continuous pass. The line is built around a full process train: uncoiler, welder, strip storage, degreasing section, continuous annealing furnace, zinc pot, air knife, skin pass mill, tension leveler, oiler, shear and recoiler — with all other auxiliary equipment required for a stable, continuous operation.
The entry section handles cold-rolled hard-state steel coil in SPCC and SPCD grades, from 0.1 mm to 2.5 mm in thickness and 650 mm to 1,650 mm in width, with coil weights up to 25 tonnes. Inside the furnace the strip is annealed and reduced in a controlled atmosphere; it then passes through the zinc pot and air knife, where coating weight is held at 60–275 g/m² double-side with ±5 g/m² adjustability. Skin pass and tension leveling deliver the flatness and surface quality needed for downstream forming, while the oiler protects the finished coil in storage and shipment.
To control running costs we specified a heat recovery system on the waste gas, which recovers heat from the furnace exhaust to preheat incoming strip and combustion air. The result is a measurable reduction in fuel consumption per tonne of coated coil without any compromise on line speed or coating quality.
Line Configuration
| Process Section | Function |
|---|
| Uncoiler & welder | Continuous coil feeding with automatic strip joining |
| Strip storage | Buffers the line during coil changeover |
| Degreasing section | Removes oil and surface contamination before annealing |
| Continuous annealing furnace | Annealing and reduction of the strip surface |
| Zinc pot & air knife | Hot-dip coating with precise coating weight control |
| Skin pass & tension leveler | Surface finish, flatness and mechanical property tuning |
| Oiler, shear, recoiler | Oiling, cutting to coil weight and finished coil take-up |
Technical Specifications
| Parameter | Specification |
|---|
| Line type | Continuous hot-dip galvanizing / galvalume line |
| Raw material | Cold-rolled hard-state steel coil, SPCC / SPCD |
| Strip thickness | 0.1 – 2.5 mm |
| Strip width | 650 – 1,650 mm |
| Coating weight | 60 – 275 g/m² (double-side) ±5 g/m² adjustable |
| Coil weight | Max 25 tonnes |
| Product grade | CQ, DQ, DDQ |
| Annual capacity | 100,000 – 300,000 MT/Y (200,000 MT/Y configured) |
| Energy saving | Heat recovery system from waste gas |
| Line functions | Annealing reduction, galvanizing, finishing, straightening |
Results & Benefits
- Galvanized coil is now produced in-house, cutting import lead times from weeks to days.
- A 200,000 MT/Y capacity base gives room to grow into regional export orders.
- Full CQ/DQ/DDQ range covers construction, HVAC, appliance and fabrication customers.
- Coating weight held to ±5 g/m² stabilised downstream forming and painting yields.
- Waste-gas heat recovery lowered energy cost per tonne of coated coil.
Conclusion
By moving from coil trading to in-house continuous galvanizing, the Malaysian service centre converted a supply-chain weakness into a competitive advantage. The line's wide gauge and width range, tight coating control and heat-recovery design make it a durable platform for both domestic distribution and ASEAN export growth.

 আপনার বার্তাটি 20-3,000 টির মধ্যে হতে হবে!